As renewable natural gas (RNG) projects become more sophisticated, gas treatment is more than just meeting pipeline specifications. It also requires understanding what happens to those contaminants as they move through the treatment process and beyond.
Halogenated volatile organic compounds (HVOCs) are a good example.
Chlorine and fluorine-containing compounds can be present in landfill gas as HVOCs. The specific compounds and concentrations vary by site.
The challenge is that these compounds can break down and form acidic and undesirable compounds within an RNG plant.
Destroying the HVOC Doesn’t Eliminate the Halogen
During catalytic or thermal treatment, carbon-halogen bonds can break, potentially converting to other halogenated compounds and/or acid species such as hydrochloric acid (HCl) or organic chlorides.
In other words, successfully destroying HVOCs doesn’t necessarily eliminate the halogens. Chlorine can reappear downstream in another, potentially more corrosive, form.
Without an appropriate removal step, acid and residual organic chloride species can reach dryers, cryogenic equipment, compressors, and other downstream assets. For owners and operators, the potential consequences include corrosion, equipment damage, unplanned maintenance, lost production, and challenges maintaining pipeline-quality gas.
Secondary reactions can create another problem. Reactive fragments may form residual organic chlorides and heavier compounds that contribute to fouling, increased pressure drop, restricted flow, or equipment failure.
Turning the Challenge into a Treatment Strategy
The limitations of conventional treatment approaches created a need for a more comprehensive way to manage halogenated compounds throughout the RNG process train.
This challenge drove innovation at SCS.
Addressing the problem starts with understanding the chemistry across the entire RNG process train, rather than halogen removal as an isolated step.
The practical approach is to characterize the incoming gas, determine how halogenated compounds will behave under the plant’s design configuration and operating conditions, remove compounds as much as possible with traditional technologies, and, if required, apply the most appropriate conversion mechanisms and capture the targeted species before they reach sensitive downstream equipment.
From Industry Challenge to Patented Solutions
At SCS, we have successfully developed practical, proven halogen treatment approaches. What was once considered impossible is now cost-effective and commercially available.
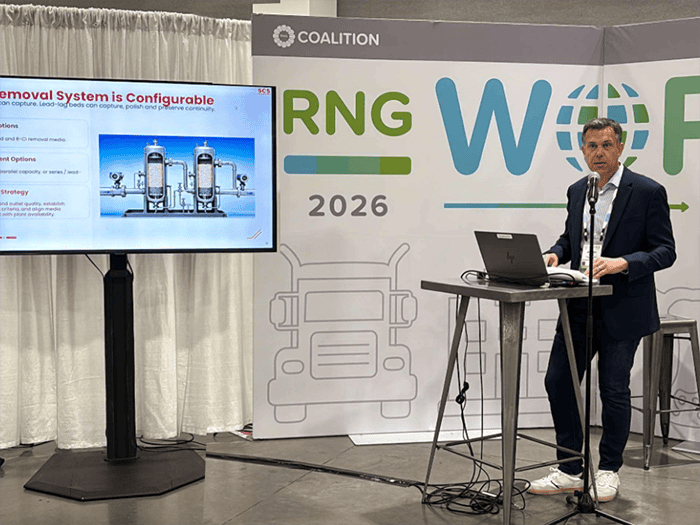
U.S. Patent 12,605,670 addresses the conversion of HVOCs into acid in wet gas, followed by solid-phase acid removal. The phased approach integrates acid removal with TSA water removal using single or multiple removal vessels.
U.S. Patent 12,496,550 uses a hydrogen source with a catalyst and/or heat to react halogen-bearing compounds and then separate the resulting acid. The approach can integrate with downstream processes such as nitrogen or cryogenic removal while also addressing secondary compounds and sulfur chemistry such as dimethyl sulfide (DMS).
Both approaches could provide a comprehensive solution to removing halogens, sulfur, and other complex organic species. Effective treatment is now possible with an appropriately designed conversion and capture system tailored to the gas chemistry and system.
The Bigger Lesson for RNG – Performance
When corrosion or gas-quality issues emerge, the answer isn’t necessarily to add another piece of equipment. Start by diagnosing the gas, symptoms, and operating conditions. Understand what is happening chemically. Then evaluate the treatment options and integrate the selected solution into the broader RNG process.
The result is a safer, more reliable facility; steady, consistent revenue; reduced avoidable maintenance; reduced downtime; and compliance with pipeline tariff gas quality requirements.
For RNG owners and operators, the key takeaways are simple:
Additional RNG Resources: